Choosing a PVC twin-screw extruder for flooring production requires more than comparing machine prices or motor power. The right equipment needs to process your PVC compound consistently, maintain stable melt flow, and work smoothly with downstream calendering, cooling, and cutting equipment. These factors influence flooring thickness, surface quality, production efficiency, and material waste.
For manufacturers planning to produce stone plastic composite (SPC) or luxury vinyl tile (LVT) flooring, start by defining the finished product, material formulation, sheet dimensions, and required output. SKY WIN provides flooring extrusion equipment designed for different PVC-based material and production requirements. Understanding these factors before requesting a quotation helps you choose a configuration that fits your factory rather than paying for features you do not need.
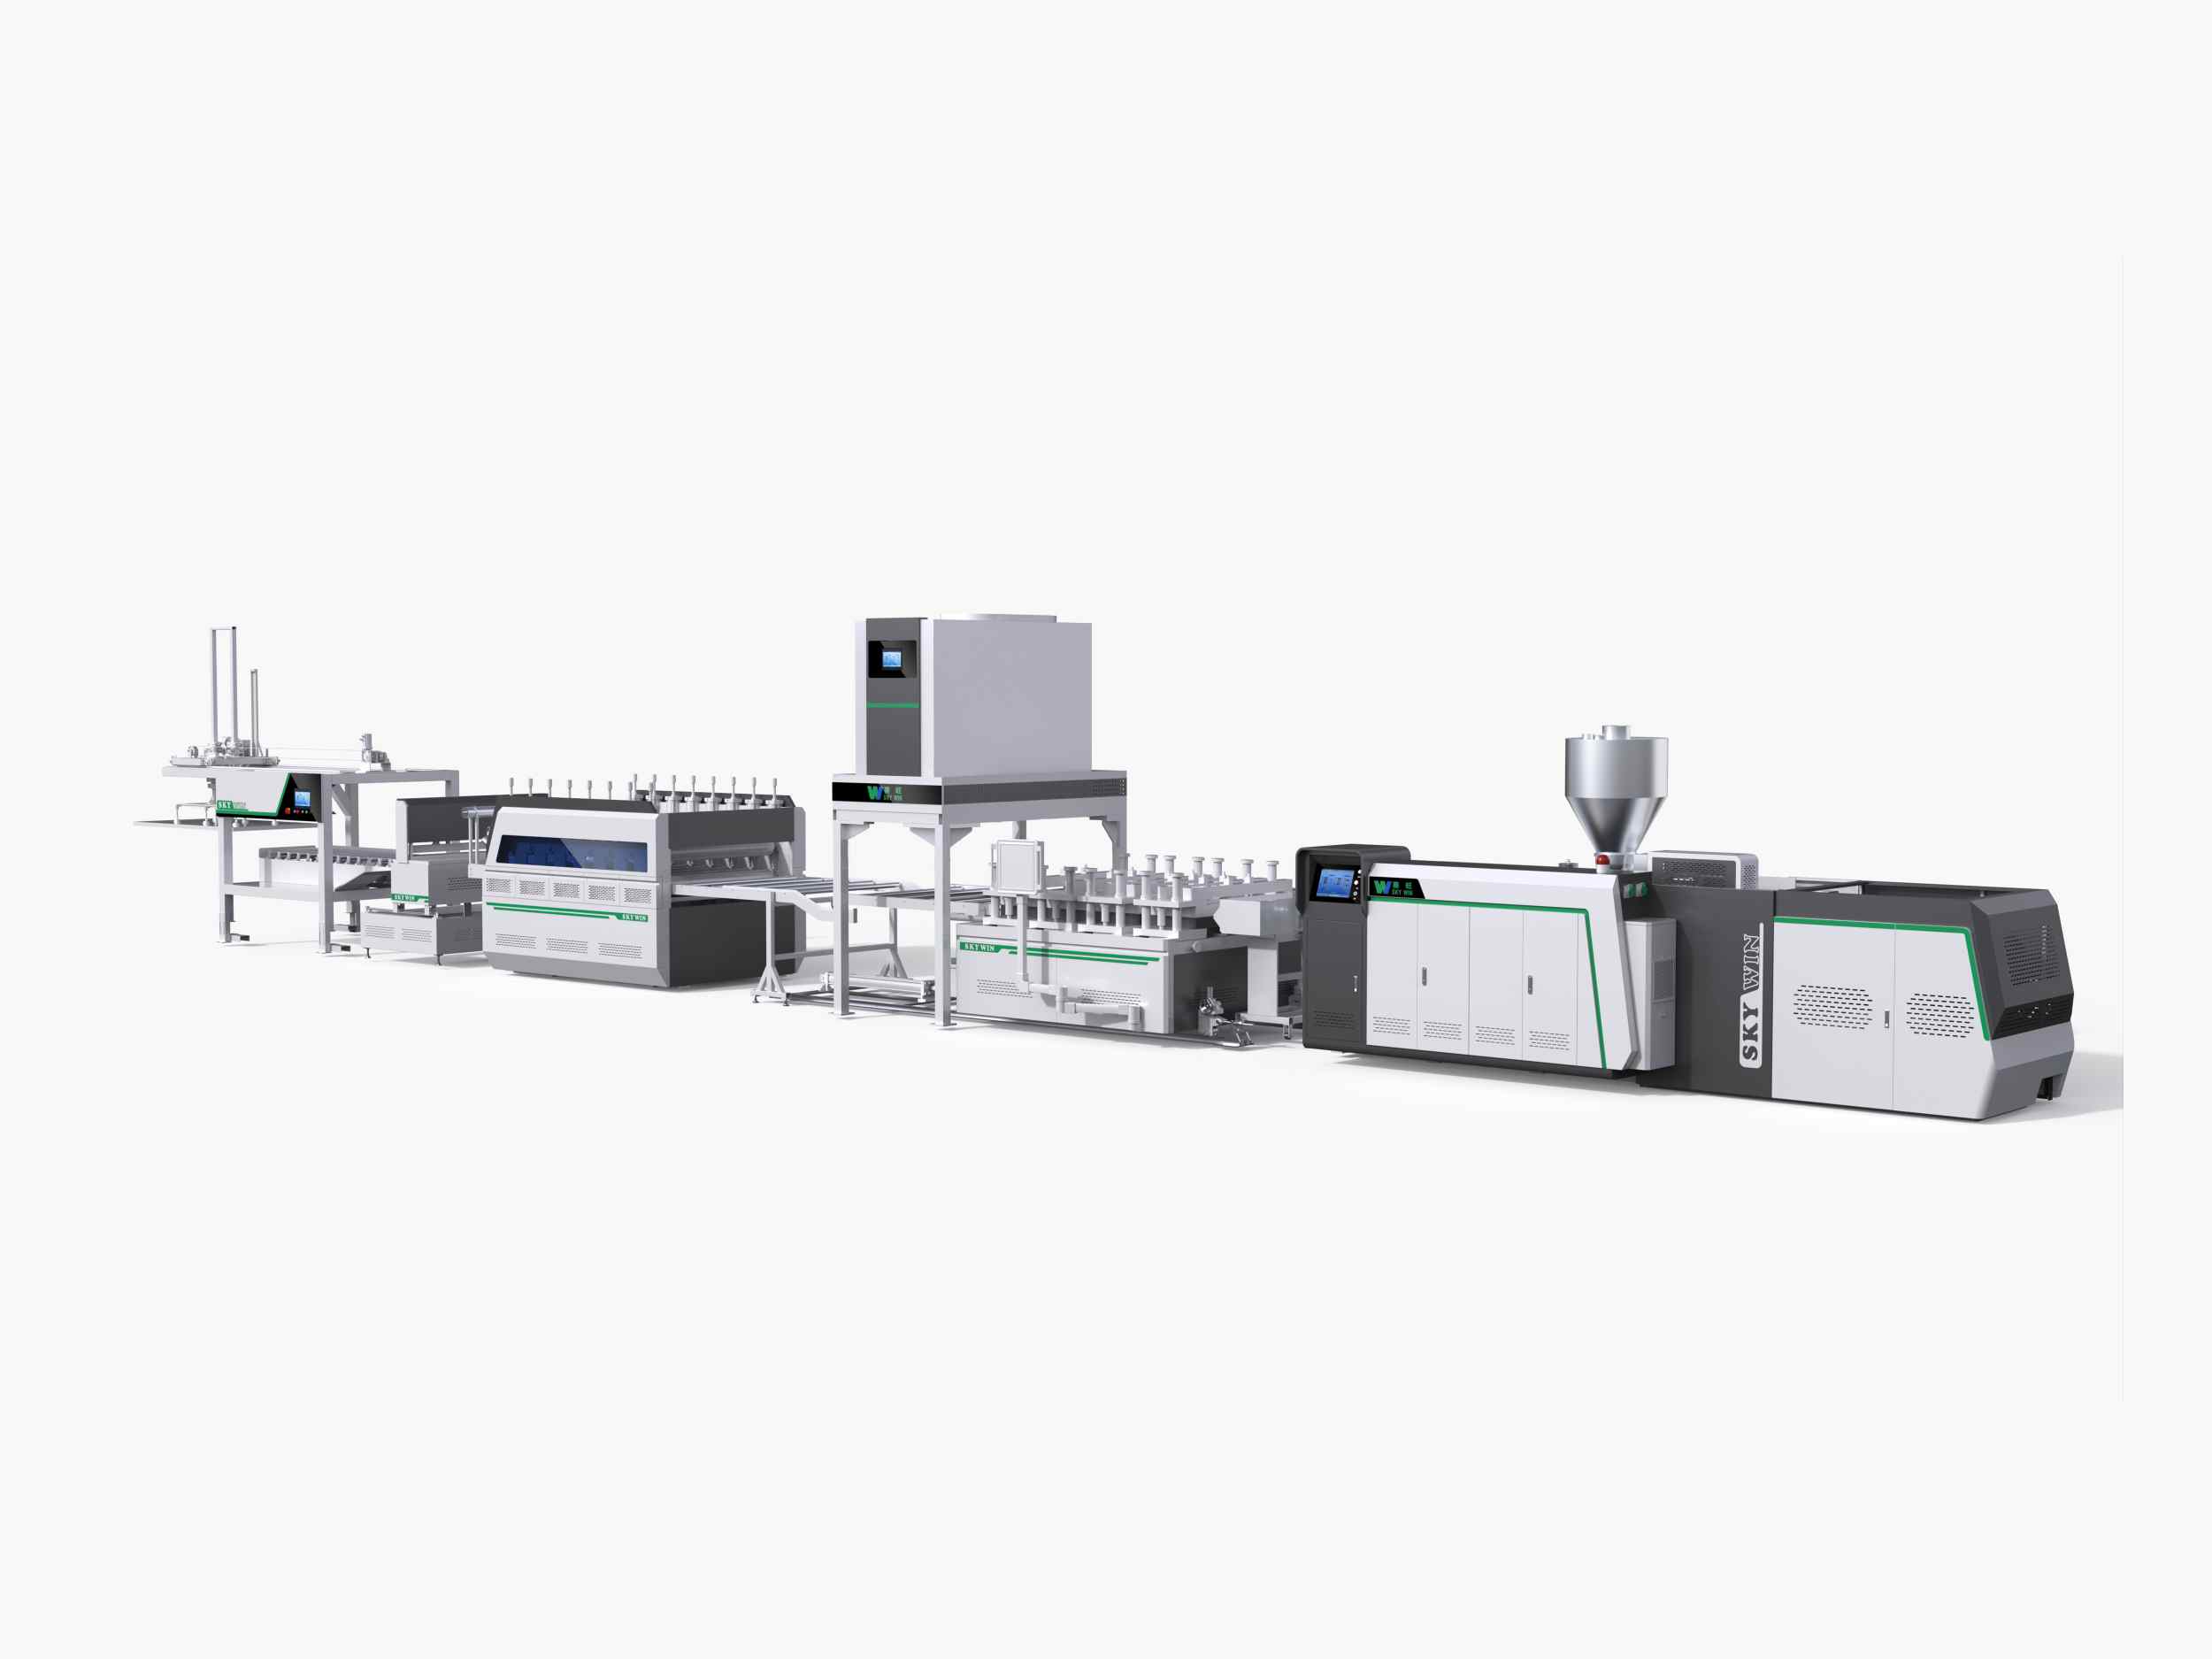
The following guide explains how to evaluate screw design, production capacity, sheet quality, and complete line configuration when selecting a PVC twin-screw extruder for flooring manufacturing.
Start with Your Flooring Product and Material Formulation
The most suitable PVC twin-screw extruder depends on the flooring product you intend to manufacture. SPC, LVT, and WPC flooring have different material compositions and processing requirements, so a machine suitable for one application should not automatically be assumed to fit another.
SPC flooring commonly uses PVC resin, calcium carbonate, stabilizers, and processing additives to create a rigid core. Its mineral filler content makes consistent feeding, effective plasticization, and wear resistance important considerations.
LVT flooring has different formulation requirements depending on its structure and flexibility. Manufacturers may need to pay closer attention to sheet handling, calendering, layer bonding, and surface finish. Double-layer LVT production also requires the extrusion system to support the intended layer structure.
WPC flooring compounds may contain wood flour or other wood-based fillers. These materials can change feeding behavior and processing requirements, so the screw configuration and operating conditions must be evaluated against the actual formulation.
Before requesting a quotation, prepare the following information:
- Flooring type and finished product structure.
- Raw materials, filler content, and processing additives.
- Target sheet width and thickness range.
- Required production output and operating schedule.
- Whether online lamination, embossing, or other finishing processes are needed.
Providing these details helps the supplier recommend a suitable configuration instead of quoting a machine based only on a general product name.
Choose the Right Twin-Screw Configuration
Screw configuration affects how material is conveyed, mixed, plasticized, and delivered to the extrusion die. For rigid PVC flooring compounds containing mineral fillers, a conical twin-screw extruder is a common configuration to consider.
SKY WIN's SPC/PVC Flooring Sheet Extrusion Line uses a conical twin-screw extruder designed for mixing, plasticizing, and continuously extruding flooring composite materials. The published product specifications list PVC resin and calcium carbonate as raw materials.
When comparing PVC twin-screw extruders, evaluate these points:
- Screw design: Confirm that the screw geometry is appropriate for the planned PVC compound and filler loading.
- Torque and drive system: Check whether the drive can maintain stable processing under the intended production conditions.
- Temperature control: Review the heating zones and control system to help maintain consistent plasticization.
- Screw and barrel wear: Mineral fillers can increase abrasive wear, making material selection, maintenance, and replacement costs important.
- Processing stability: Ask how the machine handles normal changes in formulation and operating speed.
A larger motor does not automatically mean better flooring quality. Screw design, temperature settings, feeding consistency, and downstream equipment all contribute to the final result.
Match Extruder Output to Your Actual Production Target
Rated output is an important specification, but it should not be the only basis for choosing a machine. A supplier's maximum output may not represent the production rate achievable with your particular flooring formulation, sheet dimensions, and quality requirements.
For example, a factory producing a thick SPC core with a high mineral filler content may have different processing requirements from a factory producing a thinner sheet at a higher line speed. The required output must also be compatible with the die, calendering rollers, cooling section, haul-off unit, and cutting equipment.
When reviewing output specifications, ask the supplier to clarify:
- The rated output and the conditions under which it is measured.
- The expected output for your actual material formulation.
- The sheet width and thickness associated with the quoted production rate.
- Whether downstream equipment can maintain the same continuous production speed.
- How much room the configuration leaves for future changes in production demand.
It is also useful to distinguish between the extruder's material throughput and the finished flooring output. Start-up losses, edge trimming, rejected sheets, and changes between production runs can affect the amount of saleable product produced in a shift.
For a meaningful comparison, ask every shortlisted supplier to quote against the same material formulation, sheet dimensions, output target, and equipment scope. This makes it easier to compare machine configurations and estimate the investment required.
Check Sheet Width, Thickness, and Dimensional Stability
The extrusion system must produce a sheet that meets the dimensions and quality requirements of the finished flooring. Stable melt flow helps the die distribute material consistently, while the calendering and cooling sections help control sheet thickness, flatness, and dimensional stability.
During equipment selection, confirm the following specifications:
- Minimum and maximum sheet thickness.
- Effective sheet width and the corresponding tooling requirements.
- Calender roller arrangement and temperature-control options.
- Cooling capacity and the expected production conditions.
- Thickness consistency and flatness requirements for your finished product.
These requirements are connected. Increasing extrusion output without sufficient calendering or cooling capacity can create a bottleneck and make it more difficult to maintain consistent product dimensions.
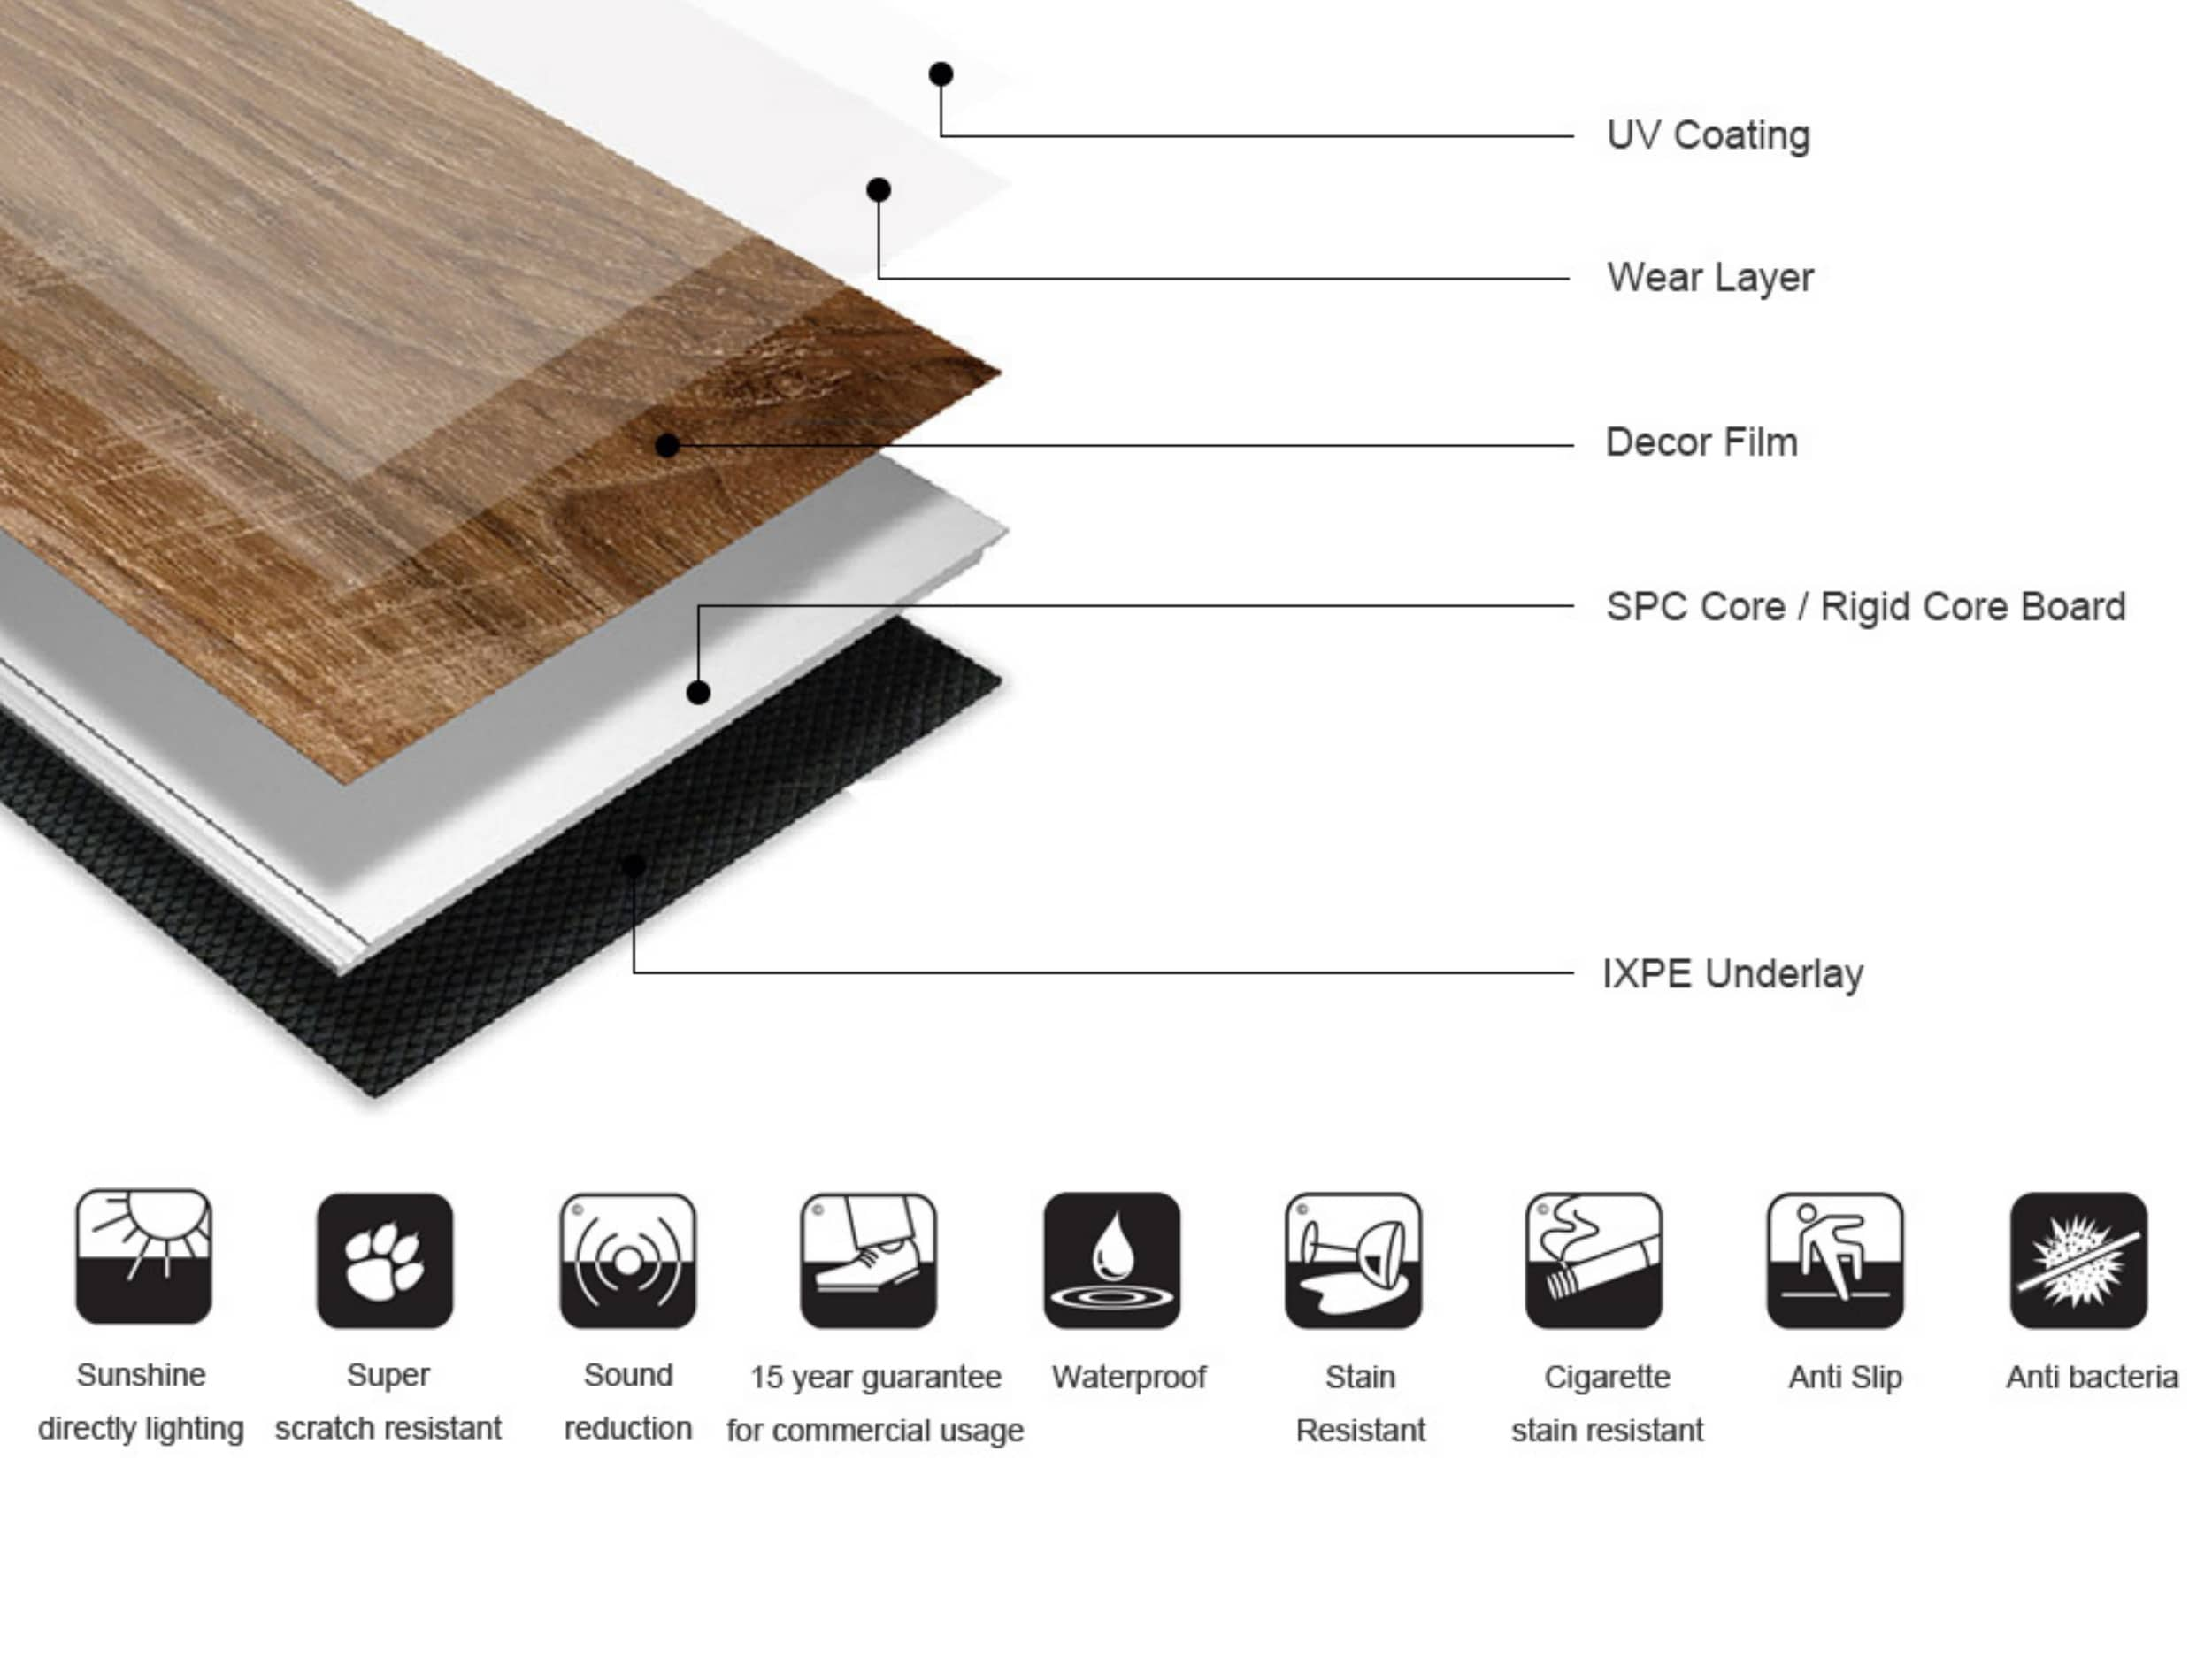
For manufacturers producing multiple flooring specifications, discuss the available adjustment range, tooling requirements, and changeover procedure before the machine is built. Do not assume that every specification can be produced on the same setup without modification.
Evaluate the Complete Flooring Extrusion Line
A twin-screw extruder is only one part of a flooring manufacturing system. Final sheet quality and production efficiency depend on how well the extrusion section works with the equipment that follows it.
A typical SPC flooring sheet production process includes material preparation, twin-screw extrusion, die forming, calendering, optional online lamination and embossing, cooling, edge trimming, and cutting. The exact configuration varies according to the finished flooring structure and factory requirements.
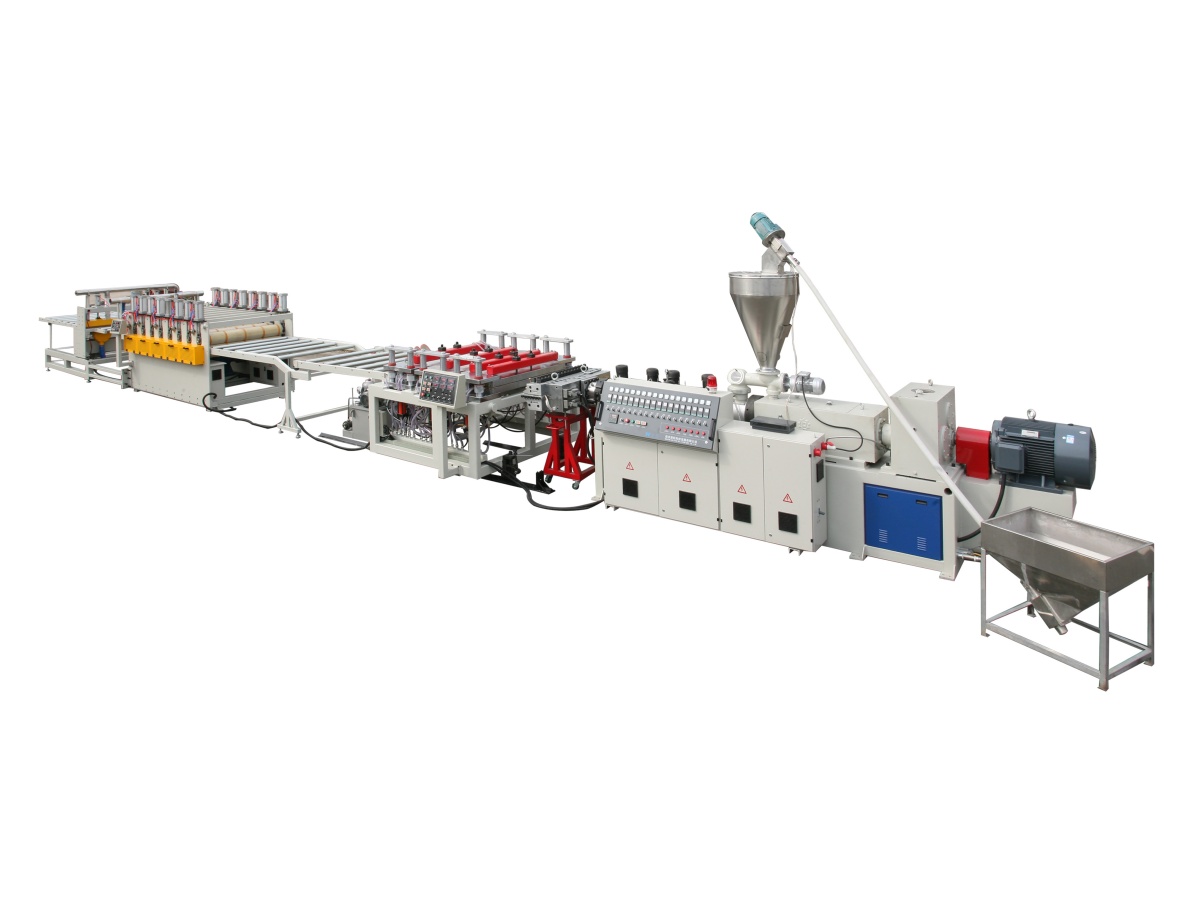
When evaluating a complete line, review the following equipment and functions:
- Feeding and material preparation: Consistent feeding helps reduce fluctuations in material supply.
- Extrusion die: The die must match the required sheet width, thickness, and material flow.
- Calendering system: The rollers help control sheet thickness, flatness, and surface quality.
- Lamination and embossing: These options may be required for integrating decorative films, wear layers, or surface textures during production.
- Cooling and cutting: Properly coordinated cooling, haul-off, and cutting help the line maintain dimensional consistency and continuous operation.
- Electrical controls: Coordinated control of the main machine and downstream equipment helps operators manage the production process.
Ask the supplier to confirm which components are included in the quotation and which are optional. This is particularly important if your production plan includes online lamination, embossing, or additional cooling equipment.
Consider Single-Layer or Double-Layer Production
Flooring structure is another important selection factor. If your product requires two layers to be extruded and combined in one continuous process, a double-layer extrusion system may be worth evaluating.
A double-layer LVT line uses separate extrusion systems to form the intended layers. The material formulation, layer ratio, bonding requirements, and downstream finishing process need to be considered together.
For this application, SKY WIN offers a Double-layer LVT Flooring Extrusion Line designed to produce two-layer LVT flooring sheets in a continuous process. The published product information describes a dual-extrusion configuration and optional online lamination.
This type of system is worth discussing if your production plan involves a two-layer structure, different formulations between layers, or integration with additional finishing processes. However, it is not automatically the best choice for every flooring factory. The final decision should be based on the product design, required output, and manufacturing cost.
Compare Energy Use, Maintenance, and Long-Term Operating Costs
The purchase price is only one part of the total cost of a PVC twin-screw extruder. Electricity consumption, replacement parts, cleaning, routine maintenance, downtime, and material waste can all affect the cost per square meter of flooring.
Before making a purchasing decision, request information about:
- Main motor power and total installed power.
- Expected energy consumption under comparable production conditions.
- Maintenance intervals and recommended spare parts.
- Screw and barrel wear protection for mineral-filled compounds.
- Availability of technical support, installation guidance, and operator training.
- Lead time, commissioning arrangements, and after-sales service.
When comparing two machines, make sure their quoted output and product specifications are equivalent. A machine with a lower purchase price may not provide the lowest operating cost if it produces more rejected material or requires frequent maintenance.
It is also useful to ask the supplier which components are standard and which are optional. This helps avoid unexpected costs when adding lamination, embossing, or automation features later.
When Should You Consider a Flooring Base Material Line?
Some manufacturers focus on producing flooring base sheets rather than completing every stage of finished flooring production. In this case, the required machine configuration may differ from a line designed for integrated lamination and finishing.
SKY WIN's PVC/WPC Flooring Base Material Extrusion Line is designed to produce base layers for SPC, WPC, and LVT flooring. Its published information describes an integrated process involving mixing, extrusion, calendering, cooling, and cutting.
This option may be relevant to factories that supply flooring substrates or manufacture base materials for subsequent processing. Before selecting it, confirm the material formulation, sheet dimensions, output requirements, and compatibility with any downstream equipment already installed in your factory.
A Practical Checklist Before Ordering a PVC Twin-Screw Extruder
Before approving a machine configuration, prepare a technical checklist and ask the supplier to confirm each item in writing. This makes it easier to compare quotations and reduces the risk of selecting equipment that does not match your production plan.
- Target flooring products: SPC, LVT, WPC, or another PVC-based material.
- Material formulation and expected mineral filler content.
- Required sheet width, thickness, and dimensional tolerances.
- Target output under the actual production conditions.
- Screw configuration, motor power, and temperature-control system.
- Die, calendering, cooling, trimming, and cutting equipment.
- Online lamination, embossing, or other optional functions.
- Energy use, wear parts, maintenance, and after-sales support.
- Installation space, electrical requirements, and commissioning schedule.
Sharing these details with the equipment manufacturer provides a more reliable basis for selecting a PVC twin-screw extruder than comparing machine specifications in isolation.
Frequently Asked Questions About PVC Twin-Screw Extruders for Flooring
What type of twin-screw extruder is commonly used for SPC flooring production?
A conical twin-screw extruder is a common option for SPC flooring because it is designed to process PVC-based compounds containing mineral fillers such as calcium carbonate. The appropriate screw configuration depends on the formulation, target output, and finished sheet requirements.
How do I choose the right output capacity for a PVC flooring extruder?
Start with the required finished flooring output, then confirm the expected extrusion rate for your actual material formulation, sheet width, and thickness. The calendering, cooling, and cutting equipment must also be capable of supporting the target production speed.
Can one PVC twin-screw extruder produce both SPC and LVT flooring?
It depends on the machine configuration, screw design, formulation, tooling, and required product specifications. SPC and LVT can have different material and processing requirements, so confirm the machine's capabilities with the supplier before planning production of both products.
Why is screw and barrel wear resistance important for SPC production?
SPC compounds often contain a substantial proportion of calcium carbonate and other mineral fillers. These materials can increase abrasive wear, so buyers should ask about screw and barrel materials, wear protection, maintenance intervals, and replacement costs.
What equipment should be included in a complete flooring extrusion line?
A typical line may include material feeding, a twin-screw extruder, an extrusion die, a calendering system, cooling equipment, edge trimming, haul-off, and cutting. Online lamination and embossing may be added when required by the flooring structure.
What information should I provide when requesting a flooring extruder quotation?
Provide the flooring type, material formulation, sheet width and thickness, target output, finishing requirements, and expected operating schedule. The supplier can use this information to recommend an appropriate configuration and confirm the production conditions.
For flooring manufacturers comparing extrusion equipment, the most effective starting point is a clear specification of the intended product and production target. Matching the screw configuration, output capacity, sheet requirements, and downstream equipment helps ensure that the selected line fits the factory's actual needs.